At the QC stations of processing plants, trucks carrying raw materials (corn, soybeans, bran) are frequently stuck outside the gates waiting for fat content analysis certificates. The testing process, which takes 4-5 hours per batch, creates a major bottleneck in the supply chain. This results in parking fees and delays in operational progress.
This bottleneck stems from the classic open-heat Soxhlet extraction method. The equipment not only wastes 100% of the pure solvent (petroleum, ether, hexane) by evaporating it, but also poses a fire hazard and is toxic to the working environment.
Therefore, automationThe food testing process adheres closely to regulations. TCVN 4327:2007This is a core solution for optimizing OPEX costs. This article analyzes the G350 Sonnen automated fat extraction solution distributed by Duc Duong, which helps recover >85% of solvent and solves the problem.Get out of the parking lot immediately.
1. Openx bottlenecks and parking congestion.
1.1 Cost of OPEX solvent leakage from the classic Soxhlet method
Classical Soxhlet open-heat extraction method with complete evaporationn 100%A significant amount of pure organic solvents are released into the air. This situation causes the lab’s monthly chemical procurement budget to balloon, hindering the goal of optimizing operating costs (OPEX).
The method for determining fat content is strictly regulated by TCVN 4327:2007 (ISO 6492:1999) for animal feed and TCVN 8136:2009 for food. Applying outdated technology not only wastes money but also exposes businesses to potential problems.Check regulations regarding food testing.strict.
(Read more: Quality control of agricultural products based on moisture content standards.)
The chain reaction diagram shows the impact from manual fat extraction to solvent OPEX loss and delivery lot congestion.
1.2 Crisis of congestion at raw material delivery truck yards
TimeManual fat content analysis takes up to 4-5 hours per batch. This excessively long waiting time causes congestion at the raw material receiving station.Raw materials (corn, soybeans, bran).
This situation caused prolonged traffic jams for trucks carrying goods outside the factory gates. Businesses had to bear the cost of parking fees and faced the risk of delays in the entire production line.
2. Automated fat extraction system recovers 85% of the solvent.
2.1 Reduce solvent usage by 85% with the Sonnen G350 Fat Extractor
Manual heating methods consume a lot of energy.from 100 – 150 mL solutiona separate environment for each sample location. This cost bottleneck is completely resolved when equipped with… G350 Fat Content AnalyzerDistributed and synchronized by Duc Duong. Sino-Sonnen China G350 Official.
6-step automation device (Ngan)(m – Extraction – Washing – Recovery – Drying – Cooling) with a condensate recovery rate of > 85%. The recovered solvent is directly reused for subsequent batches, directly reducing costs by 85%.The cost of purchasing chemicals.
| Comparison Criteria | Classical Soxhlet Extraction Method | Sonnen G350 Automatic Fat Analyzer |
| Solvent recovery rate | 0% (100% loss to the environment) | > 85% (Closed-loop condensation) |
| Batch processing time | Lasts 4-5 hours per batch | Reduced to just 45-60 minutes per batch |
| Budget for purchasing chemicals | Buy 100% new solvents monthly. | Reduce additional purchase costs by 85%. |
| Release the delivery truck. | Trucks are stuck in traffic waiting for results for hours. | Get your test ticket processed quickly, and the parking lot will be freed up immediately. |
2.2 Reduce truck parking clearance time within the same shift.
Equipped with the Sonnen G350 machine, the fat extraction time is shortened.Only 45-60 minutes per batch. SpeedThis system supports QC stations in delivering test results immediately during their shift.
As a result, the warehouse department was able to receive and release truck convoys delivering raw materials quickly. The congestion at the parking lot outside the factory gate was completely resolved.
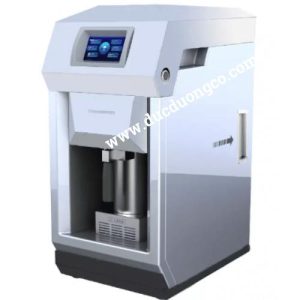
Testing food with the Sonnen G350 filling machine significantly reduces the cost of purchasing new chemicals.
3. Eliminate the loss of trace elements.
3.1 Isolating 99% of vibration frequencies using a Granite Anti-Vibration Balancing Platform
The process of analyzing fat content requires weighing the sample with precise accuracy.0.0001 g. However…However, placing the scale on a regular wooden or steel table causes the display to fluctuate constantly due to vibrations from factory machinery.
Duc Duong provides solutions Anti-vibration weighing scaleThe structure consists of a single, thick block of natural granite.
The process of absorbing and eliminating 99% of vibration frequencies in the factory environment protects the accuracy of micro-scale weighing.
The solid granite block combined with the Absorber Pad damping system absorbs and isolates 99% of vibration frequencies.It utilizes mechanical forces from the environment. As a result, the sample weighing results achieve absolute accuracy and repeatability.
3.2 Wind shield frame protects and stabilizes the weighing plate.
An independent wind shield surrounding the weighing plate helps prevent the impact of turbulent airflow in the lab. This feature allows the device to quickly establish a balanced state.
The stability of the weighing pan ensures high repeatability for sample weight measurement. Technicians completely eliminate inter-shift errors during the analysis process.
Does your company need advice on planning the automation of a food quality control (QC) station to meet ISO/IEC 17025 standards and receive a detailed ROI calculation for solvent cost savings? Click here. Contact Form for Duc Duong CompanyLet our application engineering team provide immediate support.
4. Standardization of ultrapure water by Lab QC
4.1 Eliminating background noise in the analysis with the EVO UP DIO BA System
Using traditionally boiled distilled water often results in contamination with micro-ions and microorganisms, causing background interference when preparing physicochemical or microbiological food samples. This limitation directly affects the reliability of the measurements.
To standardize the water used for sample preparation, Duc Duong distributes EVO UP DIO BA ultra-pure water filtration systemofficial channels Mirae ST Korea Official.
The water purification system achieves electrolysis.Resistivity of 18.2 MOmega.cm at 25°C and TOC index < 5 ppb. Water quality standard Class 1 according to TCVN 4851:1989 (ISO 3696:1987).) helps to completely eliminate background noise in the analysis.
4.2 Optimizing QC Station Operating Costs
The EVO UP DIO BA system helps the QC department completely eliminate the high electricity consumption costs from old boiling water distillation machines. The integrated touchscreen displays TOC and resistivity values in real time.
The automatic filter replacement alert feature helps protect equipment and ensures continuous operation. This solution optimizes the annual OPEX budget for the testing station.
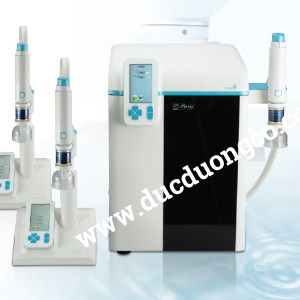
Effective food testing with the Evo-Up Dio Ba water filtration system.
5. Solutions to dispel fears of “solvent explosions”
5.1 Closed-loop air circulation eliminates EHS risks.
Lab managers’ biggest fear is the risk of fire, explosion, and asphyxiation from toxic gases like petroleum, ether, or hexane in the lab air. The Sonnen G350 incorporates a recirculation system.The sealed chamber is 100% airtight, completely eliminating the risk of solvent leakage.
At the same time, the extraction speed is 45-60 minutes.This solution alleviates concerns about trucks being fined for parking due to long waiting times for results. It ensures both EHS safety standards are met and supply chain progress is maintained.
5.2 Commitment to readily available spare parts and 24-hour on-site technical support.
To alleviate concerns about disruptions to the testing process due to equipment failure, Duc Duong maintains a genuine spare parts warehouse in Ho Chi Minh City. We always have EVO filters, temperature sensors, and replacement parts readily available.
Our team of experienced application engineers is committed to providing on-site technical support within [number] days.24 hours. This commitment ensures the factory’s QC station operates continuously without interruption.Incident.
6. The ROI problem and the ISO/IEC 17025 documentation
6.1 The ROI (Return on Investment) Problem in Under 12 Months
When presenting equipment investment plans to the Chief Financial Officer (CFO), the return on investment (ROI) ratio is important.ROI is the most compelling basis. The break-even point is calculated from an 85% saving in solvent costs plus a 100% reduction in truck parking fees.
For medium-sized QC stations, the payback period for the entire equipment investment is only 9-12 months.After this timeframe, the system will generate direct cash savings for the factory.
6.2 Standardizing the entire ISO/IEC 17025 audit documentation
Duc Duong provides a complete set of Installation Quality (IQ), Operation Quality (OQ), and Performance Quality (PQ) verification documents, along with calibration certificates. Transparent, digitized GLP data is readily available for audits.
This technical evidence makes it easier for the testing laboratory to confirm its compliance with ISO/IEC 17025 standards. Standardizing documentation helps the factory enhance its brand reputation in the market.
Conclude
In short, automationFood testing procedures onlyFat analysis is a key solution that helps factories cut 85% of wasted solvent costs and free up congested truck parking during shifts. The integrated equipment chain, including the Sonnen G350 Fat Analyzer, Granite Anti-Vibration Weighing Platform, and EVO UP DIO BA Ultra-Pure Water Filtration System, automates 6 closed-loop extraction steps, isolates 99% of factory vibration, and eliminates 100% of analytical background noise. The system completely eliminates the fear of solvent fires and explosions, eradicates parking lot parking fees, delivers a break-even ROI in under 12 months, and completes the ISO/IEC 17025 accreditation process. Duc Duong is proud to be a trusted partner distributing high-quality food QC station equipment through official channels.
Customers who require consultation on planning an automated QC station and wish to receive a quote for genuine equipment sets, please contact and register at DUC DUONG SCIENCE AND TECHNOLOGY COMPANYTo receive attentive service.
FAQ
1. By what technical mechanism does the Sonnen G350 fat analyzer save 85% on solvent costs?
The Sonnen G350 machine utilizes a 6-step automated closed-loop process (Soaking – Extraction – Washing – Recovery – Drying – Cooling). The closed-loop circulating condensation system recovers > 85% of the organic solvents (Petroleum, Ether, Hexane), allowing for direct reuse in subsequent analysis batches.
2. How does the 45-minute fat extraction speed on the Sonnen G350 machine free up delivery truck parking space?
Compared to the classic Soxhlet method which takes 4-5 hours, the G350 Sonnen machine shortens the analysis time to 45-60 minutes per batch. The QC station issues analysis reports immediately during the shift, allowing the warehouse to receive raw materials (corn, bran) and instantly relieving truck congestion outside the factory gate.
3. How does a granite anti-vibration weighing scale protect the accuracy of fat content measurements?
The solid natural granite weighing plate structure, combined with Absorber Pad damping, absorbs and isolates 99% of mechanical vibration frequencies from the workshop. As a result, the 0.0001 g micro-weighing plate does not drift or jump, ensuring accurate sample weight measurements.
4. Which country’s standards for food testing laboratories does the EVO UP DIO BA system meet?
The EVO UP DIO BA water purification system achieves a resistivity of 18.2 MOmega.cm at 25°C and TOC < 5 ppb, perfectly meeting the Class 1 Water standard according to TCVN 4851:1989 (ISO 3696:1987), completely eliminating background interference during trace analysis.
5. What documentation does Duc Duong Company provide for food QC stations to achieve ISO/IEC 17025 certification?
Duc Duong provides a complete package of Installation Quality Assessment (IQ), Operational Quality Assessment (OQ), Performance Assessment (PQ) documentation, national standard equipment calibration certification, and commits to on-site technical support at the factory within 24 hours.